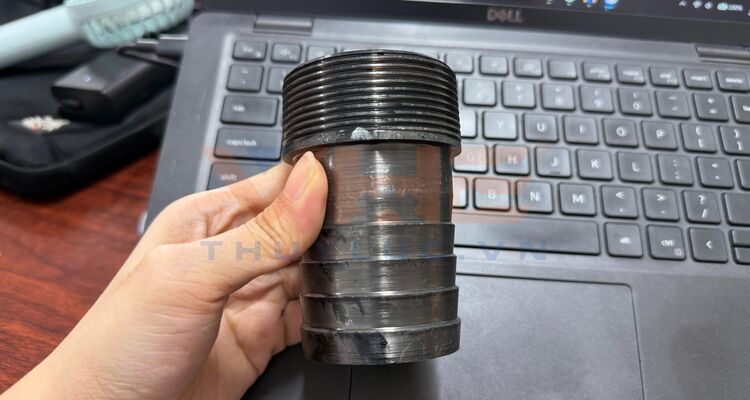
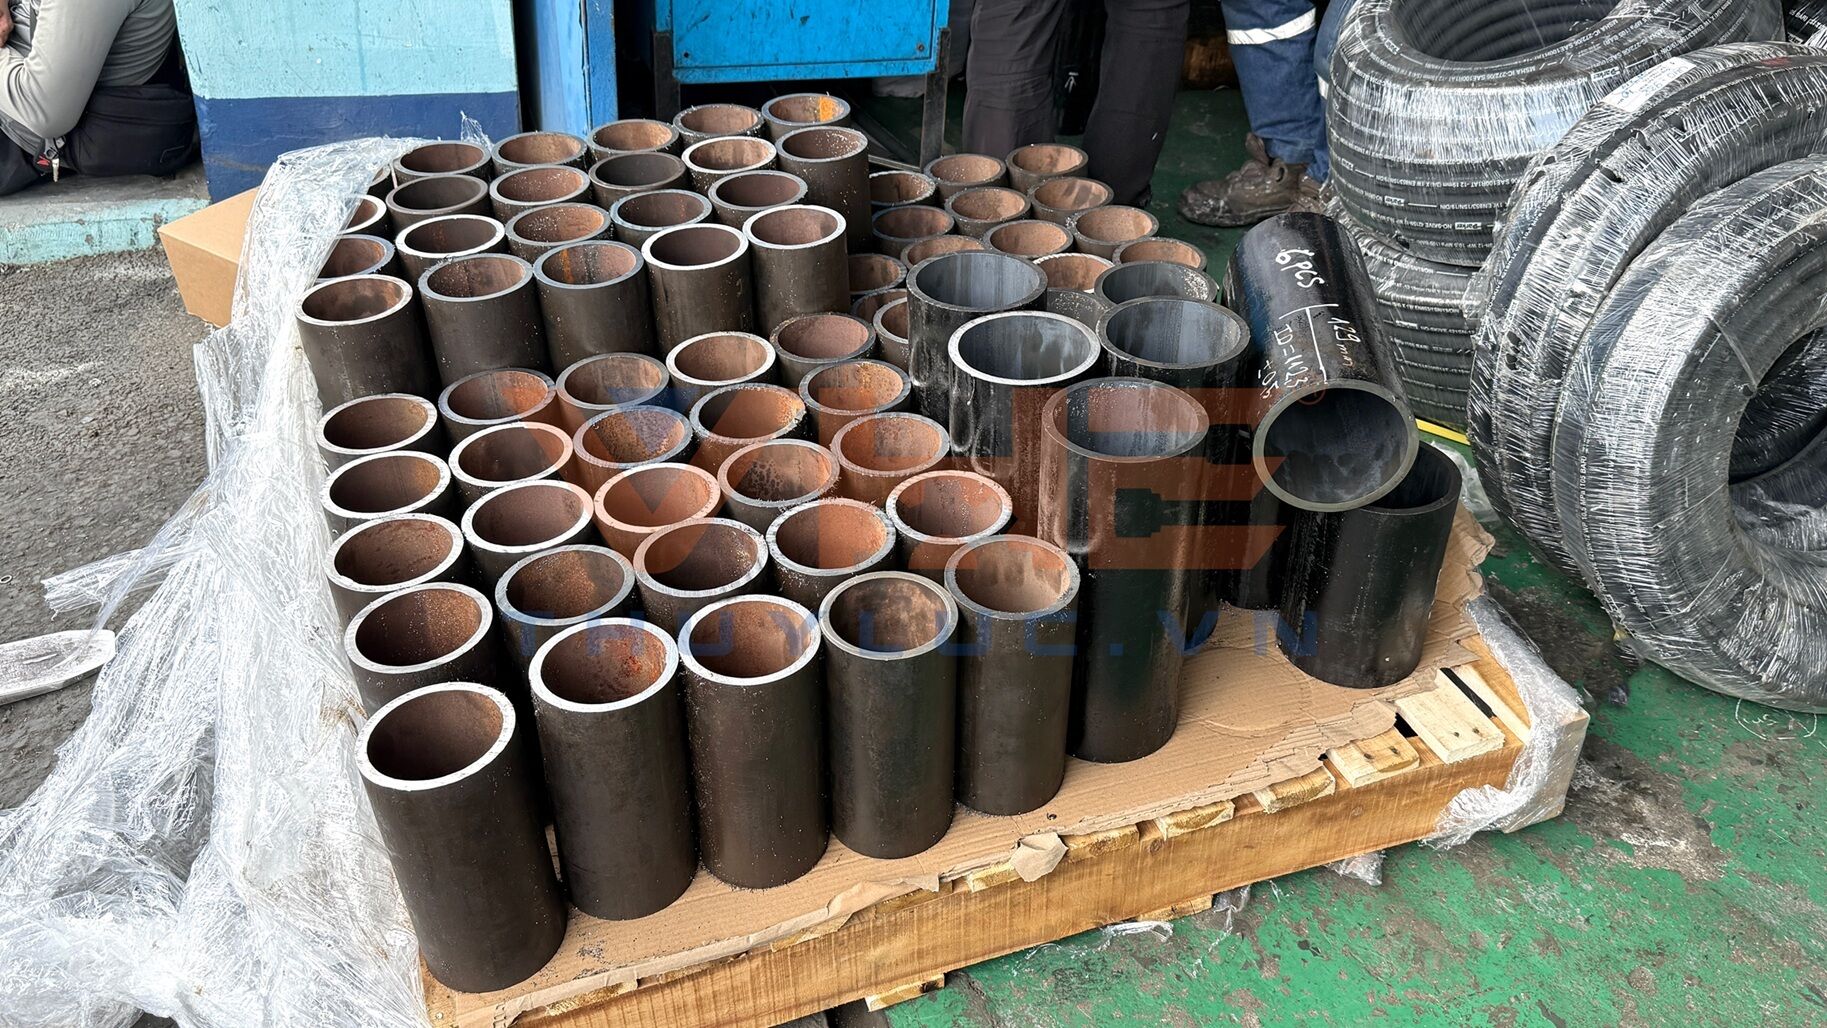
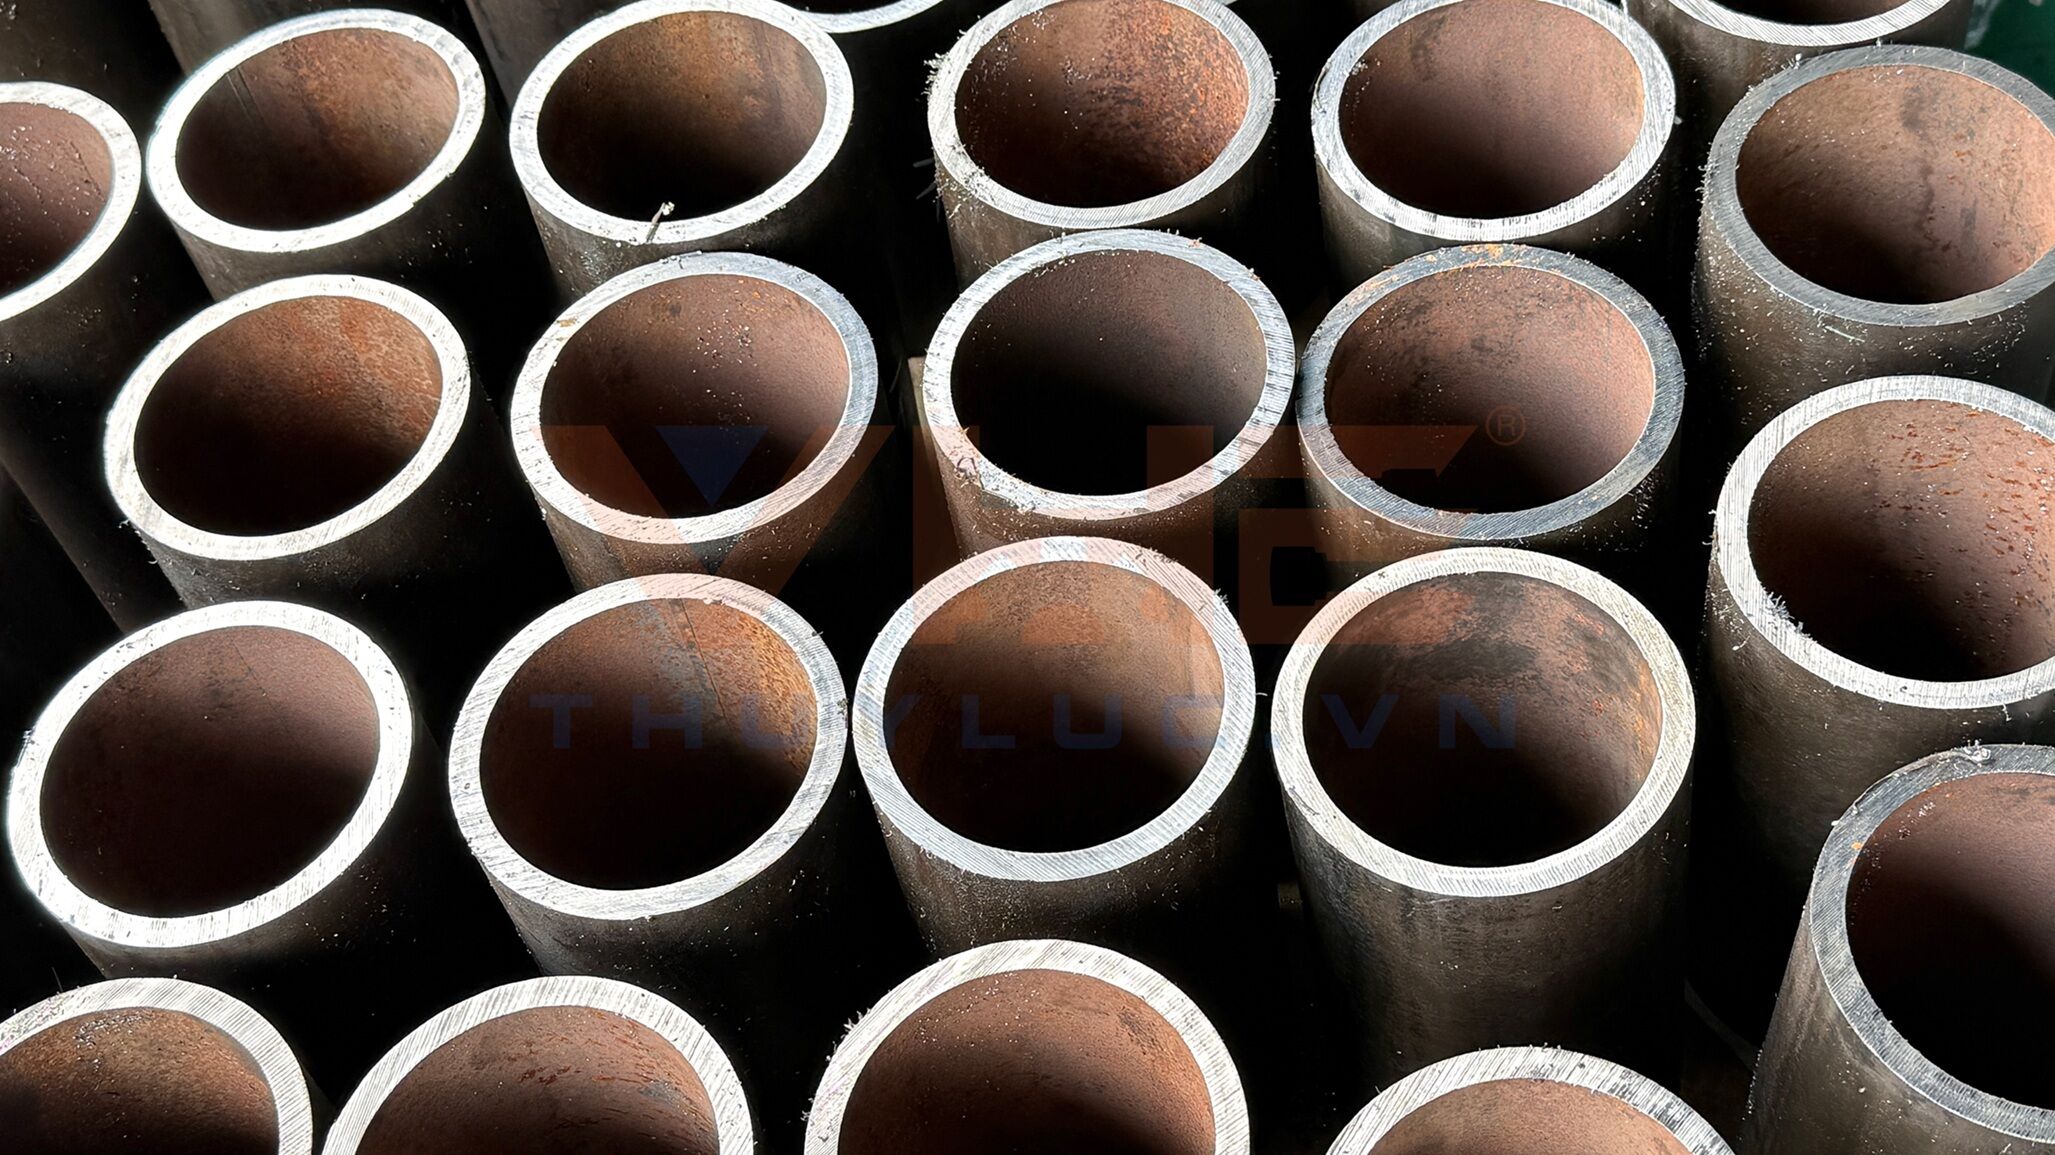
Manufacturing male threaded fittings from large-size seamless steel tube billets has long been a tough challenge for industry professionals. Recently, VHE successfully received and processed an order to crimp and reduce the ends of seamless steel tubes to 3-inch and 2-inch sizes. This prepares the billets for the customer's subsequent threading process, affirming our outstanding machining capabilities powered by a heavy-duty machinery system.
The challenge of machining large-sized fitting billets
With large seamless steel tube billets up to 3 inches featuring high hardness, crimping the ends for threading requires immense pressing force and extreme precision to avoid cracking the billet or deforming the steel structure. The majority of machining workshops in the Vietnamese market are currently equipped with only standard crimping machines, which lack the stroke and pressing force to handle these specialized steel billets.
Outstanding capability with VHE's giant tube crimping machine
Recognizing this market gap, VHE has invested in and operates a heavy-duty tube crimping system with immense pressing force. This provides a strong competitive advantage, allowing VHE to confidently take on heavyweight cases that other units struggle to execute.
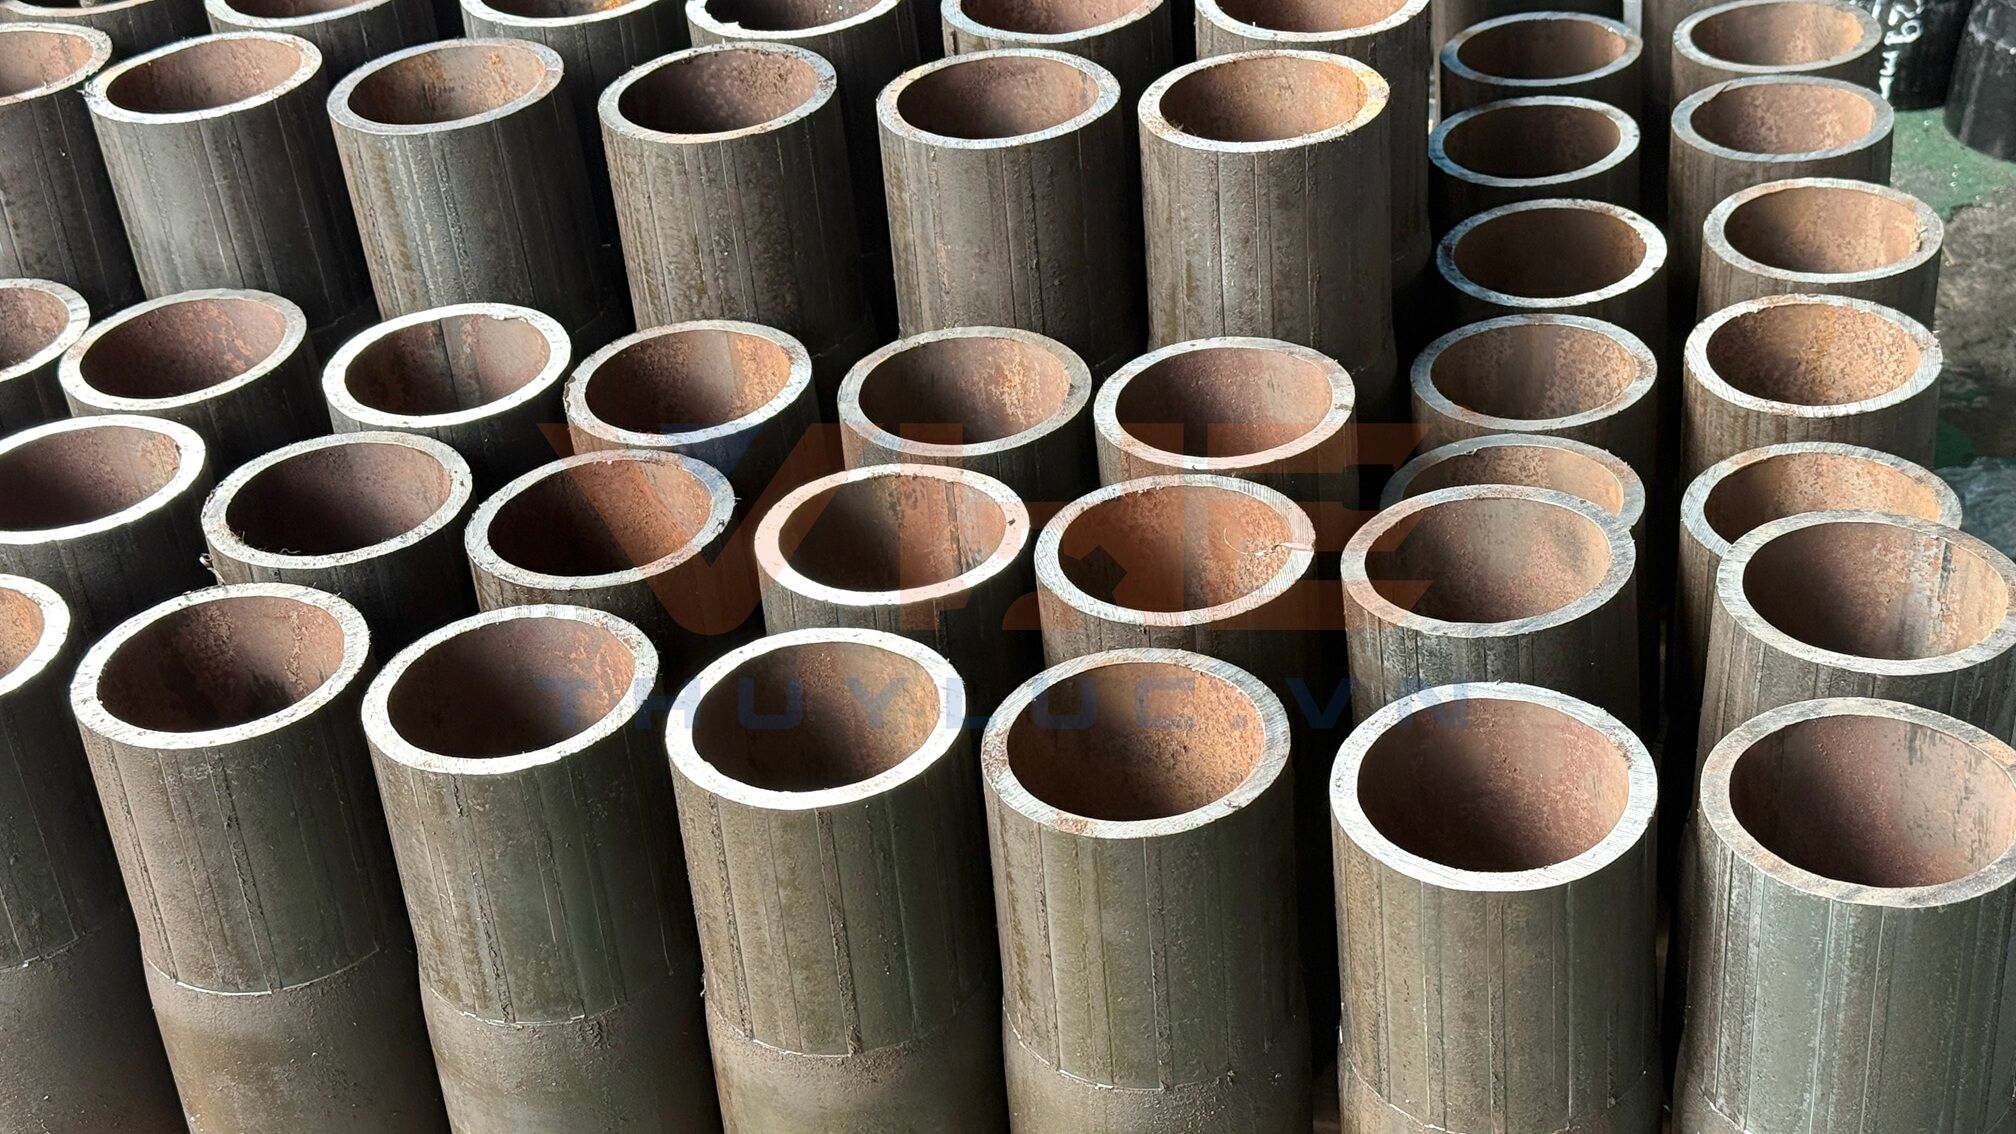
This machine features ultra-large crimping dies and a powerful hydraulic system, ensuring that the force is distributed evenly across the entire circumference of the steel tube. As a result, the 3-inch steel billet is smoothly reduced to the required ratio while retaining its mechanical properties, making it completely ready for the subsequent threading stage.
Order processing workflow for steel tube end crimping at VHE
At the VHE workshop, the machining process is strictly controlled through standardized steps:
- Receiving and preparing billets: Customers transport hollow seamless steel tubes to the VHE warehouse. (Solid steel billets require internal core boring before crimping).
- Measuring and marking: Technicians carefully measure and precisely mark the exact length of the tube end to be crimped.
- Setting up the die system: The largest specialized crimping die set is selected and installed onto the heavy-duty hydraulic crimper to match the 3-inch tube specifications.
- Executing the crimping: Each seamless tube is fed into the dies. The extreme pressing force reduces the 3-inch and 2-inch tube ends precisely to the requested drawings.
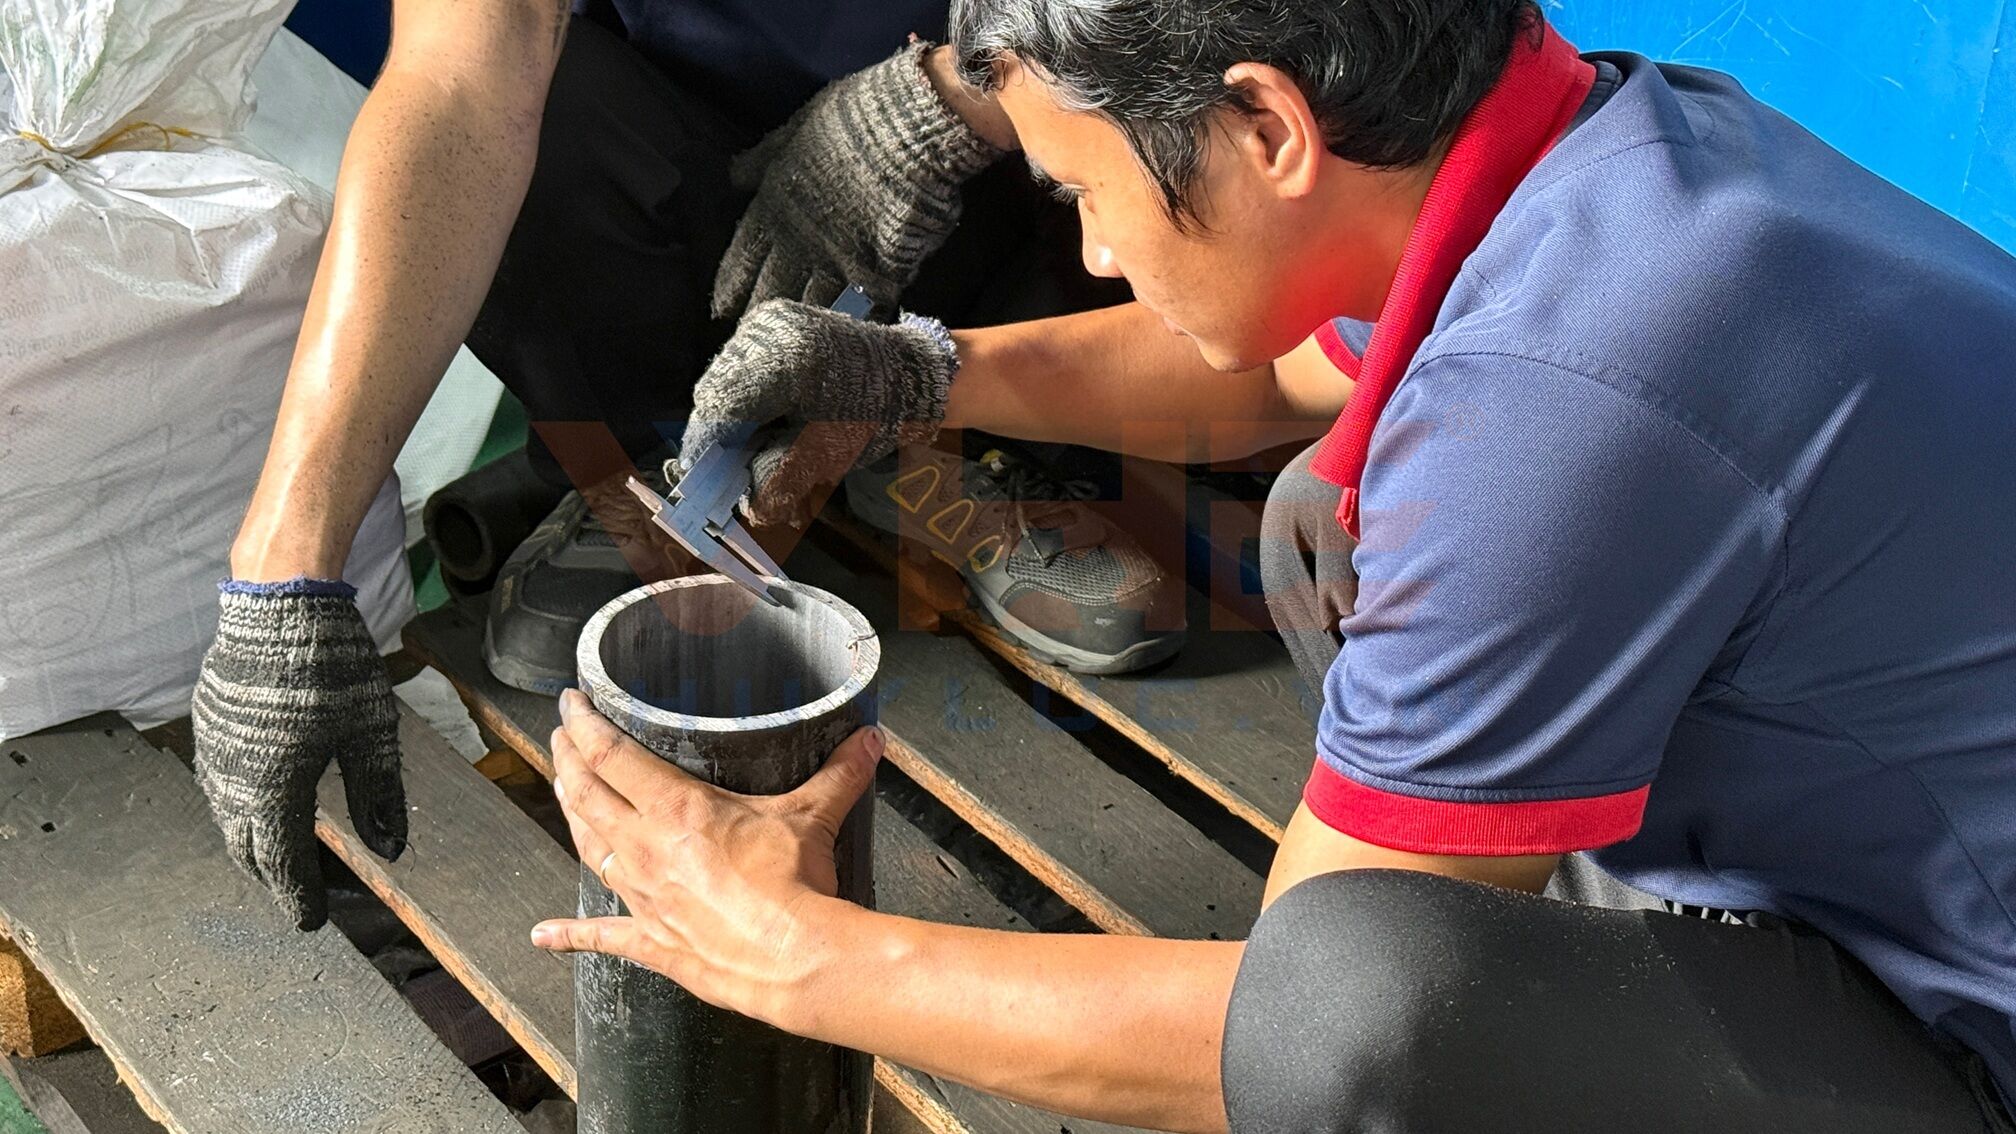
- Inspection and handover: VHE technicians and the customer use callipers to measure the tolerance of each crimp on-site, ensuring accuracy before transferring the billets for external threading.
Why choose VHE for hydraulic mechanical machining projects?
- Rare machinery infrastructure: Owning specialized large-scale tube crimping and billet pressing machines capable of handling the largest tube sizes on the market.
- Experienced technical team: Proficient operations that ensure the tightest tolerances for high-precision mechanical components.
- Transparent and secure process: Absolute confidentiality of partners' drawings and project information.
Customers and businesses in need of steel tube end reducing, threaded fitting billet processing, or specialized hydraulic mechanical solutions, please contact VHE directly for detailed technical consultation.
- Consultation & Support: 0903 067 588
- Support Email: [email protected]